CHIRON Group: machining centres, mill-turning and automation from Tuttlingen
Since 1921 CHIRON Group has been developing CNC-controlled vertical machining centres and complete manufacturing solutions for demanding milling and mill-turn processes. Around 1,600 employees at the company's own sites worldwide work on the combination that decides series production: productivity, precision, process capability and automation. What characterises CHIRON machine tools is high rigidity, thermal stability through actively cooled drive components, and loading and unloading parallel to main time – features that do not make a single cut faster, but the unit time across an entire shift.
Anyone evaluating a CHIRON milling machine therefore rarely compares travels and spindle power alone. The relevant question is: how many good parts leave the machine per shift, and how stable does that figure stay over weeks?
The CHIRON machine programme at a glance
- Micro5 and Micro5 XL – extremely compact 5-axis machining centres for small, high-value parts. Workpiece cube up to 50 mm edge length, a 5:1 ratio of machine size to workpiece, magazine for up to 60 tools and energy consumption below 500 Wh per cycle.
- Series 08 – compact centres for tolerances of a few µm and excellent surface quality, with HSK-32 or HSK-40, single- or twin-spindle, 5-axis simultaneous or as a mill-turn variant. The precision+ versions use direct linear drives.
- Series 12 – highly productive, compact and multifunctional; as single-spindle FZ 12 S or twin-spindle DZ 12 S, with mineral-cast bed, water-cooled motor spindles and 5-axis simultaneous machining.
- Series 15 – compact centres with high reliability, single- or twin-spindle, with chain or basket changer; the FZ/DZ 15 W versions with workpiece changer target high volumes.
- Series 16 – modular gantry platform for workpieces up to 700 mm and 360 kg, as FZ 16 S or DZ 16 W, with up to 162 tool pockets, the TouchLine control interface and an optional speed+ version.
- Series 18 – compact, strong, fast, with a quick basket changer, rigid table and large working area; the wheel variant covers rim sizes from 16 to 24 inches.
- Series 19 – a further step within the vertical machining centre programme.
- Series 22 – twin-spindle with 600 mm spindle spacing for large-volume components such as e-motor housings, transmission cases, oil sumps and chassis parts; with either a high-speed aluminium spindle or a high-torque spindle, optionally HSK-A100.
- Series 25 – twin-spindle with 800 mm spindle spacing for large aluminium parts such as battery trays, motor housings or structural components; as DZ 25 S with direct loading or DZ 25 P with pallet changer.
- MILL series – versatile vertical machining centres from the MILL 800 five axis to the MILL 8000 with up to 8,000 mm X travel, with swivel head, pick-up tool change and, from MILL 2000 upwards, loading parallel to main time.
- Series 715 – mill-turning in the literal sense: main and counter spindle with identical performance, complete 5-axis machining on six sides, workpieces up to Ø 300 × 1,000 mm (optionally Ø 400 × 1,400 mm), up to 176 tools, bar stock up to 102 mm.
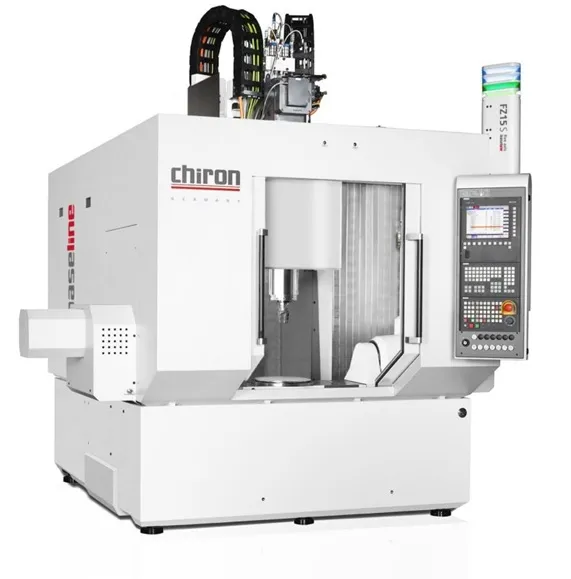
- Baseline series – preconfigured machining centres with proven technology, available at short notice; among them the FZ 15 S and MILL 800 with 5-axis capability and integrated DataLine diagnostics.
Twin spindle instead of a second machine: output per square metre
One feature runs through nearly every CHIRON series: the choice between a single-spindle and a twin-spindle version (FZ and DZ). Two spindles machine two workpieces simultaneously on the same footprint, with one control, one operator and one tool set. For unit-cost-driven series this is often a more effective lever than a higher feed rate.
When the second spindle pays off
- Batch sizes are stable and the part family is secured for years.
- Unit time is in the range of a few minutes, so setup and non-productive times weigh heavily.
- Floor space, operating staff or energy costs are limiting factors in the plant.
- Component tolerances allow two spindles to run in parallel without an additional measuring loop.
If one of these criteria is not met, the single-spindle machine – an FZ 12 S, FZ 16 S or a MILL, for instance – may be the more flexible and more economical choice. That is exactly the trade-off you can work through at the CNC Outlet Center on real machines rather than on a data sheet.
Automation and turnkey: from single machine to manufacturing solution
CHIRON combines its machining centres with its own automation solutions, enabling largely unmanned production in the third shift and at weekends:
- Feed5 – handling for automated loading and unloading of the Micro5.
- Variocell UNO – integrated automation unit in a compact format.
- Variocell MOVE – autonomous machining of small batches and complex workpieces.
- Variocell PALLET – pallet-based automation for small series and part variety.
- Variocell SYSTEM – freely configurable system for individual production environments.
In turnkey projects, CHIRON brings machining centre, tools, clamping devices, automation and process engineering together into a production-ready package: process design for the specific workpiece, validation of statistical process capability, production support during ramp-up, operator training and lifecycle services. This is complemented by the digital solutions SmartLine and SmartServices and by factory refurbishment with manufacturer know-how. Automation, clamping devices and spindles are also contributed by CHIRON Croatia under the HSTEC brand.
CHIRON machining centres at the CNC Outlet Center
The CNC Outlet Center is not the agency of a single manufacturer but a presentation and sales platform. For a six-figure investment decision this makes three practical differences.
Inspect exhibits under power instead of comparing data sheets
Every machine listed at the CNC Outlet Center can be viewed in the showroom and tested under power. Chip behaviour, noise, access to the working area, operating concept and tool change time can be assessed before an order is placed – not first at acceptance.
Stock machines: immediately available and lower in entry price
Alongside project machines, the CNC Outlet Center holds many stock machines. As a rule they are not only cheaper to acquire but above all available at short notice. Anyone who needs capacity for an order already won gains months this way. That matches the logic of the CHIRON baseline series, which is designed precisely for short delivery times with proven technology.
Examine alternatives before you invest
The CNC Outlet Center carries machines from many manufacturers. Even when a particular CHIRON series already seems settled, a direct comparison with alternatives is worthwhile – especially for investments above €100,000. Often it is not the choice of manufacturer that shifts, but the specification: one series larger, one spindle more, a different tool magazine.
Peripherals and accessories in combined offers
The CNC Outlet Center works with numerous peripheral and accessory manufacturers – from chip conveyors and coolant treatment through extraction and metrology to clamping devices and tool presetting. When these components are considered together with the machine, combined offers with discounts often become possible that separate procurement would not produce.
Narrow down the direction here, detailed design by CHIRON
An initial project discussion at the CNC Outlet Center helps with the fundamental decision: flexible single machine, manufacturing concept with integrated automation, or turnkey project. Workpiece-related process design, validation, commissioning, production support, training and lifecycle service remain with CHIRON.
Replacement investment: have your existing machine valued independently
If an existing machine is up for replacement, the CNC Outlet Center can value it independently and include it in the overall calculation. Residual value, disposal and transition period then become part of the investment case instead of an open item beside it.